Global layout

 +86 769 2366 8529


Time:2026-09-24 Views:16
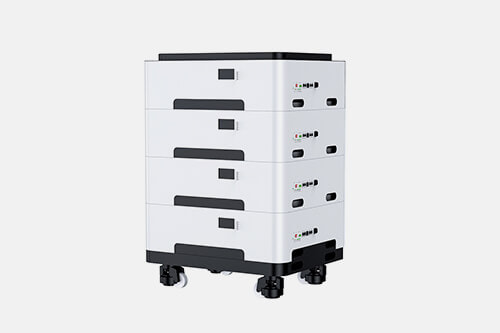
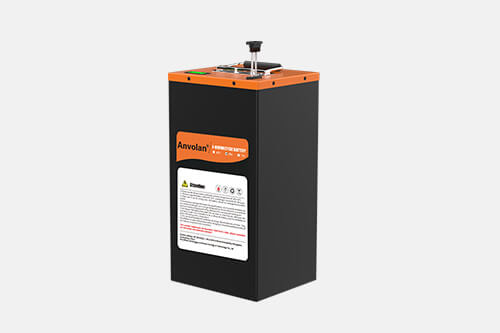
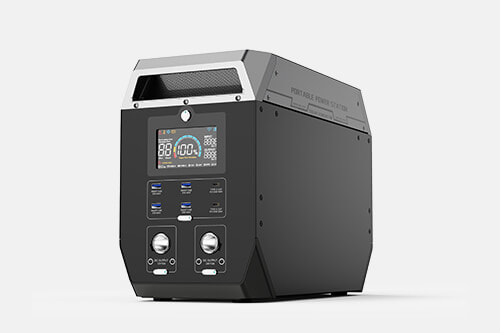
Short-distance urban travel has given rise to a variety of two-wheeled transport vehicles. Featuring compact size, flexible operation, convenient parking and economical energy consumption, these vehicles are widely used for urban commuting, campus patrol and short-distance delivery. As the core component of the whole vehicle, the power energy storage unit directly determines the driving range, safety performance and product reputation. Under the global trade landscape, an increasing number of brand owners, cross-border traders and vehicle assemblers no longer merely purchase standard finished goods. Instead, they adopt private label customized manufacturing. Relying on the R&D and production capacity of professional factories, they develop energy storage products marked with their own brand logos. This cooperation model helps brand owners achieve product differentiation, flexibly control product specifications, packaging and technical parameters, build unique product positioning in segmented markets, and has become a rapidly rising business model in the industrial chain of two-wheeled commuter vehicles.
The core logic of private label manufacturing is that manufacturers complete the production, inspection and labeled delivery of energy storage products according to customers’ technical requirements, appearance design and packaging plans. Brand owners take charge of market positioning, channel sales and brand promotion, while production is undertaken by manufacturers with mature production lines and stable cell supply chains. Compared with purchasing ready-made standard products, private label manufacturing delivers remarkable differentiated advantages. Brand merchants can adjust the capacity, voltage, shell structure and BMS protection strategy of energy storage products according to local market regulations, vehicle parameters and user habits. Whether it is compliant versions for European and American markets, or reinforced versions suitable for high-temperature regions such as Southeast Asia and the Middle East, targeted design adjustments can be made to escape homogeneous low-price competition and lift product premium potential.
When selecting manufacturing partners, the overall capability of the factory is the key factor affecting project success. First, the stability of the factory’s cell supply chain needs to be evaluated. The quality of energy storage products is built on cell raw materials. Reliable manufacturers maintain diversified cell procurement channels and conduct multi-dimensional incoming inspections on capacity, internal resistance and cycle stability to avoid later failures caused by inconsistent cell performance. Second, the automation level of production lines and process control system are critical. The assembly of energy storage units involves multiple processes including cell sorting, series-parallel arrangement, welding, protection board integration and sealing packaging. Automated production lines reduce errors caused by manual assembly and guarantee consistent parameters among bulk products. For export goods, batch stability directly affects overseas return rates and brand reputation.
Product safety and compliance certification are indispensable core links in private label manufacturing projects. Different countries and regions have independent regulations on electrical safety, transportation and environmental protection for energy storage products. Exported goods must pass corresponding safety tests and certifications for smooth customs clearance and market access. Professional manufacturers can assist customers in preparing certification documents and sample testing, and adjust product design to meet standards of target markets, avoiding risks such as cargo detention or return due to non-compliance. In addition, the factory’s internal reliability testing capacity matters greatly, including high-low temperature cycling test, vibration test, waterproof and dustproof test, overcharge and short-circuit safety test. Only after complete reliability verification can products adapt to complex outdoor working environments across regions and reduce potential safety hazards in end use.
Custom development capability differentiates ordinary processing plants from professional private label manufacturers. Basic OEM only replaces labels and outer packages; in-depth customization covers shell mold opening, wiring harness adjustment, modification of protection strategies and development of communication interfaces. Brand customers have diverse requirements. Some clients need adjusted battery housing shapes to fit the installation dimensions of specific vehicles; others intend to add intelligent monitoring functions to realize remote data transmission of battery level and fault early warning. Manufacturers with independent R&D teams can support customers in scheme design, sample prototyping and repeated test iteration, forming a complete workflow from sample verification to mass production. For new brands and startup traders, there is no need to build independent R&D and production lines. By leveraging manufacturing resources, they can quickly launch self-branded products and greatly cut R&D investment and trial-and-error costs for new items.
Supply chain delivery management is another priority under private label cooperation. Cross-border orders are often characterized by strict delivery deadlines and volatile order volumes. Brand owners need to assess the factory’s production flexibility, raw material inventory management and logistics support. During peak sales seasons, order volume surges in a short period, and manufacturers must have sufficient capacity to respond rapidly. In off-seasons, small-batch trial orders can be supported to facilitate customers’ market testing. Meanwhile, packaging belongs to customized private label content. Customers can customize color boxes, user manuals and anti-counterfeit marks printed with their own brand LOGO and product parameters. Factories should package products strictly following customers’ packaging specifications to maintain brand image and reduce package damage during cross-border transportation.
Quality control and after-sales collaboration lay the foundation for long-term stable cooperation. Manufacturing projects should not only focus on shipment volume; a full-process quality traceability system is essential. Production records and inspection reports are kept for each batch. Once quality problems occur in overseas terminals, manufacturers can quickly locate production links and analyze root causes. Factories must implement comprehensive pre-shipment inspection. Every energy storage unit is fully tested for voltage, internal resistance and protection functions before delivery to prevent nonconforming products from entering the market. For after-sales service, both parties need to agree on fault judgment criteria, repair plans and spare parts supply mechanisms in advance. Cross-border after-sales cycles are long with high logistics costs. Clear after-sales agreements can reduce subsequent commercial disputes and maintain brand owners’ service capability in overseas markets.
From the perspective of market trends, the global two-wheeled commuter vehicle market keeps expanding, and demand for self-branded products from customers in different regions continues to rise. Small and medium brand owners and cross-border sellers can hardly afford huge investment to build their own factories. The private label model effectively lowers market entry barriers and enables more participants to launch exclusive products. At the same time, market requirements on safety standards, service life and intelligence of energy storage products keep rising. The living space for simple low-price labeling is shrinking. Manufacturers capable of providing solution design, certification support, stable delivery and full-lifecycle quality control will gain more cooperation opportunities. Only deep collaboration between brand owners and manufacturers to polish products can build long-term advantages amid fierce global competition.
In summary, private label manufacturing is a mature and efficient industrial cooperation form in cross-border trade of energy storage products. This model realizes professional division of labor for brand operation, sales and production, allowing each side to exert its strengths. When selecting manufacturing partners, brand merchants should comprehensively evaluate the factory’s cell supply chain, production technology, certification capability, custom development strength, delivery flexibility and after-sales quality system, instead of merely focusing on quotations. With support from professional manufacturers, brand owners can rapidly launch self-branded energy storage products, accurately meet vehicle requirements and regulatory standards of overseas markets, create differentiated products, expand global sales channels, and continuously explore market opportunities in the energy storage track for urban two-wheeled commuter vehicles.
Be the first to receive our latest news, how-to user guides,
and exclusive deals! Subscribe now.

 Headquarter Address:10F, Building 25, N0. 179 Fengguan, Dongshen Road, Dongguan, Guangdong
 Factory Address:Building 3, Area D, Shengyang Science and Technology Industrial Park, East District of Suichuan County Industrial Park, Ji'an, Jiangxi
 Headquarter Telephone No.:+86 769 2366 8529
Factory Telephone No.:+86 796 6111618
 Contact Person:Kevin Chen
 Email Address:chen@xpower-world.com