Global layout

 +86 769 2366 8529


Time:2026-09-14 Views:192
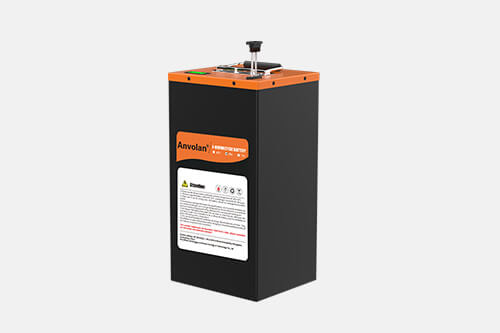
Against the backdrop of continuous expansion of the global energy storage market and explosive demand in application scenarios such as residential energy storage, commercial & industrial energy storage, RV and yacht power supply, off-grid photovoltaic systems, and industrial backup power supplies, 200Ah lithium iron phosphate high-capacity batteries have become mainstream products in the energy storage market thanks to outstanding features including safe stability, long cycle life, low self-discharge rate and high energy conversion efficiency. There are numerous battery suppliers on the market, yet most of them are trading intermediaries. Only a handful of manufacturers are original factories capable of independent R&D and in-house production of 200Ah LiFePO4 high-capacity batteries. As an original manufacturer, we abandon the simple assembly and OEM model. We achieve full industrial chain control from cell R&D, material selection, BMS system development, structural design, full-process quality control to finished product testing. Relying on multi-dimensional core advantages, we supply highly reliable 200Ah high-capacity lithium iron phosphate batteries for global customers and support the implementation of the global green energy storage industry.
Product performance advantage is the fundamental pillar for a 200Ah high-capacity LiFePO4 battery factory to stand firmly in the market. Unlike some products on the market with falsely marked capacity and shrunk parameters, our factory’s 200Ah lithium iron phosphate batteries adopt Grade A LiFePO4 cells to guarantee true rated capacity from the source, with stable actual discharge capacity and no false capacity labeling. The LiFePO4 material features high thermal stability and low risk of thermal runaway. Compared with lithium ternary batteries, it delivers superior safety performance under acupuncture, extrusion and high-temperature conditions, making it ideal for long-duration continuous energy storage applications. The cells are optimized through special formula adjustment, achieving more than 6000 charge-discharge cycles. Under regular operating conditions, the service life of the battery can reach about ten years, far exceeding ordinary products in the industry. Meanwhile, the battery maintains an excellent discharge platform with steady continuous current output and small voltage fluctuation, ensuring stable operation of loads such as photovoltaic energy storage, RV power and industrial equipment. The low-temperature performance of the battery is specially calibrated, greatly improving capacity retention in cold environments. It can operate stably in high-altitude regions and cold northern areas. The low self-discharge characteristic reduces power loss during long-term static storage, making it suitable for backup power scenarios, where sufficient power can be retained after long storage. Before delivery, every set of our 200Ah high-capacity batteries strictly sorts cells by capacity, internal resistance and voltage consistency. The voltage difference between cells is controlled within a tiny range, which greatly slows down battery degradation and extends the service life of the whole energy storage system.
Self-developed BMS battery management system serves as a key core advantage that distinguishes our factory from ordinary assemblers. Many small and medium assembly factories directly purchase generic BMS protection boards with simple functions and rough protection logic. Such boards are prone to protection failure and communication abnormalities when high-capacity batteries work under long-time high-current conditions. As an original factory, we independently develop an intelligent BMS system specially adapted to 200Ah high-capacity LiFePO4 batteries, with in-depth algorithm optimization for heavy-duty energy storage working conditions. This intelligent BMS integrates multiple protection mechanisms, including overcharge protection, overdischarge protection, overcurrent protection, short-circuit protection, high-temperature and low-temperature protection. It monitors the voltage, temperature and current of every cell string in real time and triggers protection immediately once abnormalities are detected, eliminating safety risks at the software level. The BMS supports balancing management functions, performing active balancing on cell voltage differences continuously to keep all cells in synchronized condition during long-term operation and effectively slow down battery aging. Optional RS485, CAN and Bluetooth communication modules are available to realize data interaction with inverters, photovoltaic controllers and host computers. Users can check real-time battery status including remaining capacity, temperature and charge-discharge data for intelligent management of energy storage systems. Both hardware and software of our self-developed BMS are independently debugged and developed. Custom function development can be carried out according to customer scenario requirements to match inverters and energy storage systems of different brands, a technical advantage unavailable for pure traders.
A full-link quality control system is our core advantage to guarantee stable mass product quality. Once batch quality defects occur in high-capacity batteries, they will bring huge safety risks and economic losses to energy storage projects. Therefore, strict quality management is an indispensable capability for original factories. Our factory establishes full-process quality inspection standards covering raw material incoming inspection, cell screening, production assembly, aging testing and finished product verification. At the raw material warehousing stage, all LiFePO4 cells, separators, electrolyte, enclosures and BMS circuit boards need incoming quality inspection. Unqualified raw materials will be returned directly to suppliers and forbidden to enter the production workshop. Before cells are put on production lines, secondary sorting is carried out. Only Grade A cells with well-matched capacity, internal resistance and voltage can be used to manufacture 200Ah high-capacity batteries. In the assembly process, fully automatic laser welding technology is adopted to form uniform and firm welding spots and avoid hidden risks such as virtual welding and cold solder joints caused by manual welding. After assembly, batteries must go through aging stations for long full charge and full discharge cycle aging to simulate real working conditions and screen batteries with potential defects in advance. Before delivery, finished products will undergo a complete set of reliability tests: waterproof and dustproof test, shock and compression resistance test, high-low temperature cycle test and short-circuit safety test. Products can only be labeled, stored and shipped after passing all tests. All testing equipment is self-matched. Complete test reports are retained for each batch of products, with traceable product information. Third-party sampling inspection is supported to meet quality audit requirements of overseas customers.
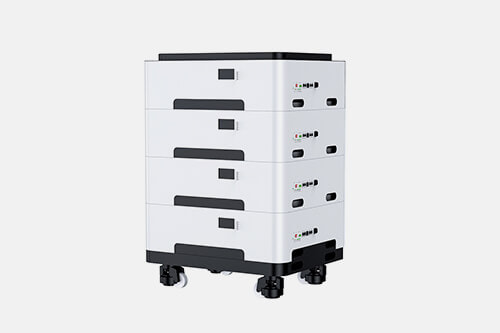
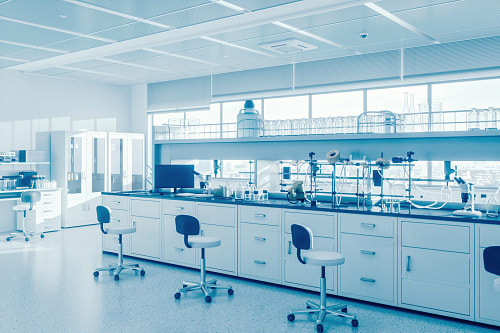
Flexible R&D and customization capability is our prominent advantage to serve diversified global markets. Energy storage application scenarios are highly differentiated. Customers from different countries and projects have varied requirements for 200Ah high-capacity batteries. Traders can only provide ready-made standard spot goods without in-depth adjustment, while our factory owns R&D laboratories and flexible production lines to respond quickly to customized demands. On the hardware side, we can adjust battery enclosure material, protection grade, dimension specifications and terminal types. On the software side, we can customize BMS protection parameters, communication protocols and Bluetooth functions. The products support multiple installation solutions including wall-mounted, stackable and floor-mounted types to fit residential energy storage, commercial and industrial energy storage, marine, RV, communication base stations and other scenarios. We support OEM and ODM services, custom brand logos, outer packages and user manuals as requested by customers. Meanwhile, the R&D team continuously iterates products, follows the technical trends of the energy storage industry, optimizes battery energy density, safety structure and temperature control solutions, and launches upgraded versions of 200Ah LiFePO4 high-capacity batteries. Whether customers need sample testing, small-batch trial orders or large-scale mass orders for major energy storage projects, the factory can arrange production flexibly and deliver promptly.
Complete certification system and global compliance capability are our important advantages to explore overseas markets. For the global energy storage market, compliance certifications of battery products are the entry ticket to enter markets of various countries. Batteries produced by many small factories lack complete certifications and face risks of customs detention and failed customs clearance during export. Our factory’s 200Ah LiFePO4 high-capacity batteries have obtained a full set of international certifications, including CE, UL, RoHS, MSDS, UN38.3. They satisfy import standards of most countries and regions such as the EU, North America, Australia, Southeast Asia and the Middle East, and support multiple logistics modes including sea and air transportation. The factory produces products in accordance with ISO quality management system. Workshop environment, production workflows and warehouse management all comply with standardized specifications of the new energy industry. All exported products are equipped with complete documents including test reports, certification certificates and sea transport appraisal certificates, helping customers clear customs smoothly and reduce compliance risks in international trade. Meanwhile, the factory builds a standardized warehousing system with constant-temperature storage environment for cells and finished batteries to prevent battery performance damage caused by high temperature and humidity and guarantee stable performance of shipped products.
Professional technical service and full-cycle after-sales support constitute the factory’s core service advantage. We do not merely sell batteries, but deliver complete technical support solutions for energy storage power systems. At the pre-sales stage, technical engineers provide professional suggestions on battery selection, system matching and capacity configuration according to customers’ project operating conditions and assist customers in designing energy storage system schemes. During sales, we supply technical documents and installation guides, communicate with customer engineering teams and answer questions on product docking. After sales, a rapid response mechanism is established to provide remote technical support for product usage problems. The original factory communicates directly with customers, eliminating multi-layer markup and delayed information transmission caused by middlemen. R&D engineers can respond to technical questions directly. Supported by a mature supply chain, the factory provides long-term spare parts supply guarantee. Battery accessories and BMS spare parts can be supplied for a long time to meet operation and maintenance demands of energy storage systems.
Looking ahead, as a professional manufacturer of 200Ah LiFePO4 high-capacity batteries, we will continuously exert our full-chain advantages of an original factory, keep investing in R&D, optimize battery safety structures, iterate intelligent BMS algorithms, and improve quality control and production systems. Adhering to the philosophy of safety priority and quality-oriented manufacturing, we will keep supplying cost-effective, safe and long-life 200Ah LiFePO4 high-capacity batteries for global energy storage customers, and work with partners to promote the sustainable development of the global clean energy storage industry.
Be the first to receive our latest news, how-to user guides,
and exclusive deals! Subscribe now.

 Headquarter Address:10F, Building 25, N0. 179 Fengguan, Dongshen Road, Dongguan, Guangdong
 Factory Address:Building 3, Area D, Shengyang Science and Technology Industrial Park, East District of Suichuan County Industrial Park, Ji'an, Jiangxi
 Headquarter Telephone No.:+86 769 2366 8529
Factory Telephone No.:+86 796 6111618
 Contact Person:Kevin Chen
 Email Address:chen@xpower-world.com